What is a gummy counter, and how do you choose one? A gummy counter is the machine that fills each bottle with an exact number of gummies, and specifying one well comes down to three things: how it handles your coating, how its accuracy is actually measured, and what your real annual volume is. This guide covers all three, plus the specifications that genuinely differ between suppliers.
Key Takeaways
- A gummy counter fills each bottle by counting whole pieces, not by weighing them, so the number on the label matches what is inside.
- Well-run optical counters hold ±0.02–0.03% accuracy — but only when gummies arrive single-file, with no doubles or clumps.
- Sticky, sugar-sanded and oil-coated gummies are the hardest to count. The fix is mechanical design, not a more sensitive sensor.
- A rated 80 bottles per minute is a test-cell figure. Plan your line around 75–80% of it once changeovers and rejects are real.
- Specify the counter by coating first, bottle format second, and target annual volume third.
What Is a Gummy Counter?
A gummy counter — also written gummy counting machine — is an automatic filling system that counts individual gummy pieces and releases an exact quantity into each bottle. Instead of dosing to a target weight and accepting whatever piece count lands inside, it works in whole units: fifty gummies in, fifty gummies out, bottle after bottle.
That distinction matters most for gummies. The two things a buyer checks first — pieces in the bottle, and what the label claims — have to agree exactly, and count-based filling removes the recount rejects that plague weight-dosed lines.
Where it fits in a gummy packaging line
Counting never runs alone. It sits downstream of everything that makes the gummy and upstream of everything that closes the bottle: cooking and depositing, cooling, curing or drying, sanding or oiling, then unscrambling, counting, desiccant insertion, capping, sealing, labeling and cartoning.
The consequence is blunt: a counter is only as accurate as the product reaching its hopper. If gummies leave the dryer tacky, or carry loose sugar dust out of the sander, even the best counting head will mis-feed. Our gummy packaging overview shows how these stages chain together — and when a new counter underperforms, the cause is more often upstream than in the machine.
Counting vs weighing: two ways to fill a gummy bottle
A weighing filler doses until the target net weight is reached; a counter releases a fixed number of pieces. Weighing tolerates irregular shape and surface stickiness, and suits loose candy or bulk formats where no piece count is claimed. Counting wins whenever the count is the claim — which is most bottled gummy vitamins. Serious lines often run both: an automatic counting machine for count-claimed SKUs, a multihead weigher for bulk formats.
How a Gummy Counter Works, Step by Step
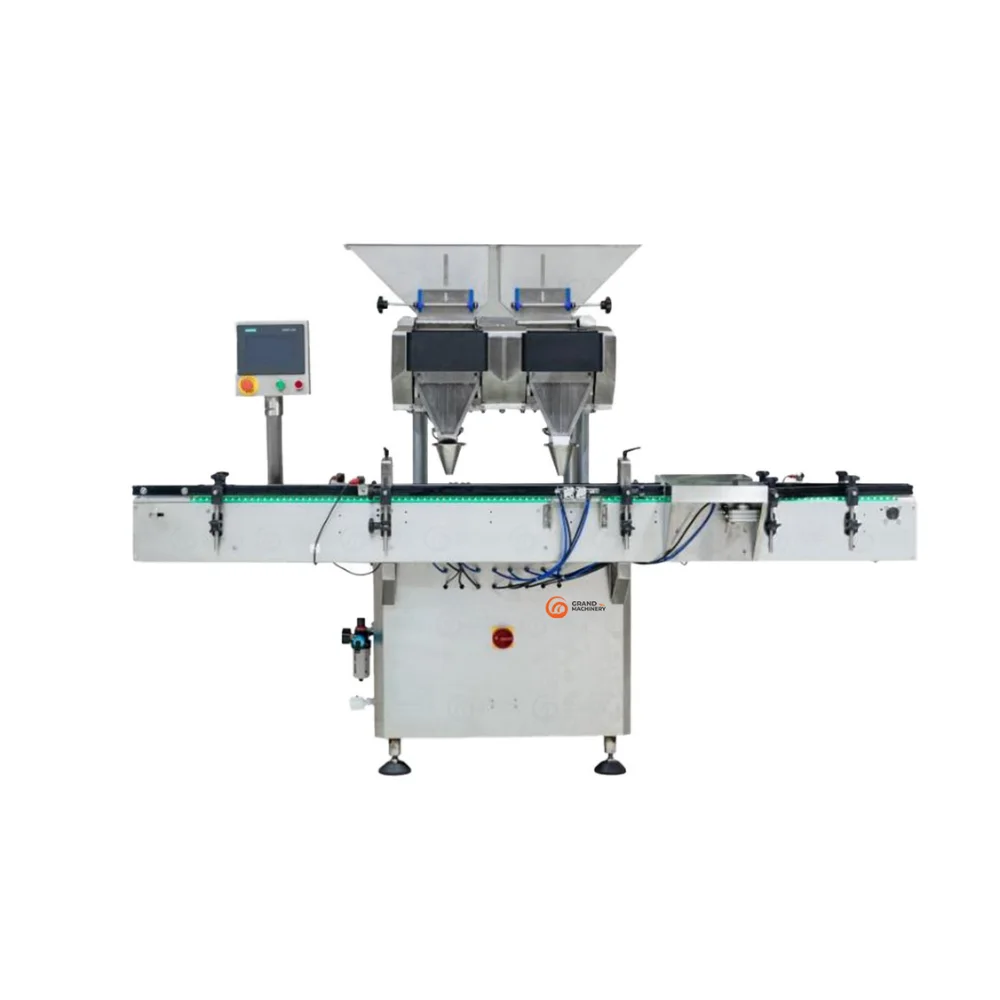
Every optical counter, whatever its brand, performs the same four jobs in the same order. Understanding them tells you where a machine can be expected to lose accuracy.
Feeding and de-clumping at the hopper
Product is lifted from the hopper to a spreader plate, which breaks up massed product and presents a thin, even blanket of gummies rather than a pile. Anti-stacking rollers and vibratory spreaders do the work; an uneven blanket is a problem every downstream stage inherits.
Single-file separation in vibratory channels
Gummies drop into parallel vibratory channels — often 12, 16 or more. Amplitude and frequency are tuned so each piece travels alone, with a clear gap to the next. A second gate rejects doubles and the rare piece riding on top of another.
Channel count is the first specification that separates one counter from another, and it scales directly with throughput. Our GM8AE automatic counting machine runs eight channels at 180,000–240,000 pieces per hour; the GM12AE runs twelve at 240,000–360,000 pieces per hour; the GM16AE runs sixteen.
Read the fine print on what those figures were measured with. All three are rated on round tablets, capsules or softgels in the 3–13 mm band — hard, dry, dimensionally stable product. A soft gummy of the same diameter does not travel the same channel at the same rate, so treat a tablet-based pieces-per-hour number as an upper bound, not a gummy specification.
GM8AE on a bottling line
Ratings are measured on tablets and capsules. Bring your own gummies to confirm the achievable rate during a factory acceptance test.
Watch on YouTubeOptical counting and batch release
At the end of each channel a photoelectric sensor or camera registers each occlusion. When the accumulated total reaches the set count, the controller closes the gates and releases the batch as one clean slug.
Bottle indexing and hand-off to capping
A star wheel or indexing conveyor positions an empty bottle under the discharge cone, triggers release, and moves the filled bottle to the capping station. Synchronisation between conveyor and gates is what keeps counts repeatable at speed.
Why Gummies Are Harder to Count Than Tablets
Tablets are flat, hard, uniform and dry. Gummies are none of those things — the single biggest reason a specification that works for tablets can fail on a gummy line.
Sticking, stacking and doubles
Soft gelatin and pectin gummies deform under their own weight and stick on contact. On vibratory channels this produces stacks of two or three pieces travelling as one, which the sensor reads once and the bottle receives twice. PTFE-coated and polished channel surfaces, plus correctly tuned anti-stacking rollers, are the countermeasures.
Sugar, oil and powder residue on the sensors
Sanded gummies shed sugar, oiled gummies leave a film, and starch-moulded gummies carry powder. All three accumulate on sensor windows and channel floors, gradually reducing detection until the machine starts undercounting — so a short, tool-free cleaning routine is a design requirement, not routine housekeeping.
Shape, size and coating variables
Bears, rings, worms, stars, drops and cubes behave differently in the same channel. Small, rounded pieces separate easily; large, flat or elongated pieces bridge. Coatings change friction, which changes the amplitude setting that works — so a counter matched to one SKU shape needs retuning to run another well.
Gummy Counter Accuracy: Reading the Numbers Correctly
Vendors quote accuracy as a percentage, and the numbers look interchangeable. They are not.
How accuracy is measured on a production line
Accuracy is the deviation between the count requested and the count delivered, sampled across many bottles. A claimed ±0.02% sounds negligible until you express it as pieces: on a 90-count bottle, that is about 1.8 pieces across a hundred bottles — roughly 0.018 pieces per bottle on average. Accuracy figures only hold at batch level, so ask over how many bottles the number was measured. Test protocols differ between suppliers, and a run on freshly dried, perfectly uniform gummies will not represent a Tuesday-afternoon production run.
What actually causes miscounts
In practice, miscounts come from a short list: doubles and stacks passing as one piece, channel overload from over-fast feed, dust blinding a sensor, static holding pieces at a gate, and product arriving damp. Every one is mechanical or process-driven — software cannot recover a piece that was never seen separately.
Accuracy targets for regulated supplement markets
For bottled supplements sold in regulated markets, a single miscount in one bottle is a labelling failure, not a rounding error. Serious buyers therefore specify count accuracy and reject verification: a checkweigher or second count downstream, plus a documented cleaning interval that keeps the claimed figure true across a full shift. Our guide to packaging for supplements covers the compliance context in more detail. Ask for the cleaning cycle time, not only the headline accuracy figure. In the US, the count printed on the label is a net quantity declaration under FDA 21 CFR 101.105.
Gummy Counter vs Weighing Filler: How to Decide
| Factor | Gummy counter | Weighing filler |
|---|---|---|
| Unit of dosing | Whole pieces | Net weight |
| Best when | Count is the label claim | Weight is the claim, or product is irregular |
| Typical accuracy | ±0.02–0.03% of count | ±0.5–2% of weight |
| Speed | 40–100 bottles/min, depending on lane count | Similar, but slower to settle at small piece weights |
| Sticky or clumped product | Needs anti-stick design | More forgiving |
| Cost of error | One piece short = one reject | Variance absorbed inside weight tolerance |
| Changeover to a new shape | Retune, sometimes channel reset | Recalibrate only |
When piece count is a label claim
Most bottled gummy vitamins state a count: 60 gummies, 90 gummies, 120 gummies. That single sentence makes a counter the only correct choice. A weighing filler that hits net weight on average will still produce bottles short by one or two pieces — and those bottles are non-conforming regardless of what the scale says.
When net weight compliance comes first
Where regulation is expressed as net weight (in the US, checked against NIST Handbook 133), or where product is loose candy sold by weight, a weigher is simpler and cheaper to run. It also handles a wide size distribution better, because it never needs the pieces to be identical.
Running both formats on one line
Many contract packers and multi-SKU brands run a weighing unit and a counting unit on one line, fed from a common bottle unscrambler. Changeover then means selecting the right filler and recipe, not rebuilding the line — a layout worth designing in at the start rather than retrofitting later.
Capacity Planning: From Bottles per Minute to Annual Output
Machine ratings are quoted in bottles per minute (BPM). Buyers budget in bottles per year. The gap between those two numbers is where most over- and under-investment happens.
Reading a BPM rating correctly
A rated figure is measured on a warm machine, with one SKU, ideal product and no interruptions. Your line will not run there. Standard practice is to plan at the normal operating speed while keeping roughly 20% headroom for recovery and surge — so an 80 BPM machine is realistically a 60–65 BPM machine across a real shift.
Conversion table: BPM → shift output → annual output
| Rated BPM | Planning BPM (80%) | Bottles per 8h shift | Bottles per year (2 shifts, 300 days, 85% OEE) |
|---|---|---|---|
| 40 | 32 | 15,360 | 7,800,000 |
| 60 | 48 | 23,040 | 11,700,000 |
| 80 | 64 | 30,720 | 15,700,000 |
| 100 | 80 | 38,400 | 19,600,000 |
Assumptions: 480 min per shift, two shifts, 300 working days, 85% overall equipment effectiveness after changeovers, cleaning and stoppages.
Choosing lane count and machine count for your target volume
Work backwards from the annual volume your sales plan needs, then check whether one machine at your bottle size can carry it. If it cannot, you have three levers: add lanes, extend shifts, or add a second machine. A second, smaller machine is often more flexible than one large unit, because it keeps a SKU running while the other handles changeover and cleaning.
Matching the Counter to Your Gummy Coating
Coating is the variable buyers underestimate most. The same counter that fills sugar-sanded bears beautifully can jam on oil-waxed softgels. Match the machine to the surface first.
| Coating type | Anti-stick requirement | Typical failure if unmatched |
|---|---|---|
| Sugar-sanded / sour-coated | PTFE channels, sugar-dust extraction, short cleaning interval | Sugar build-up blinds sensors; gradual undercount |
| Oil-coated / waxed | Polished stainless contact, de-static ionisation, gentle amplitude | Pieces slide and overlap; doubles pass as one |
| Starch / powder-coated | Dust extraction at hopper and channel exits | Powder films gate faces; gates stop sealing cleanly |
| Uncoated (plain gelatin) | Cool, dry air at the hopper; anti-stacking rollers | Surface tack causes bridging and stacks |
| Pectin / sugar-free soft | Reduced vibration amplitude, wider channel gaps | Pieces deform and bridge on narrow channels |
Sugar-sanded and sour-coated gummies
Sugar and acid sanding give the best grip for channel transport but the worst dust load. Specify dust extraction at both the hopper and the channel exit, and agree a cleaning interval you can actually hold during production. Our sugar coating guide covers how the coating stage affects downstream handling.
Oil-coated and waxed gummies
Oil and wax reduce friction, so pieces slide faster and overlap more readily. Lower the amplitude, add de-static ionisation, and rely on polished contact surfaces rather than coarse ones.
Pectin, sugar-free and soft formulations
Pectin and sugar-free gummies are softer and deform more under vibration. Wider channel gaps and gentler amplitude keep them separated without crushing them. If you produce both gelatin and pectin SKUs, say so at quotation stage — the channel set is not always the same.
Specifications to Compare Before You Buy
| Specification | What to look for |
|---|---|
| Number of channels | 8–24; match to target BPM, not to marketing copy |
| Product size range | Confirm it covers your smallest and largest SKU (commonly 3–40 mm) |
| Count accuracy | Ask how it was measured, on what product, over how many bottles |
| Rated vs operating BPM | Demand the operating figure at your bottle size and count |
| Contact materials | 304 stainless standard; 316L for aggressive acid coatings |
| Changeover time | Minutes to switch shape and count — get it in writing |
| Cleaning time | Target under 15 minutes for a full channel and sensor clean |
| Air and power | Confirm pressure, consumption and electrical supply on site |
| Verification | Downstream checkweigher or second-count option |
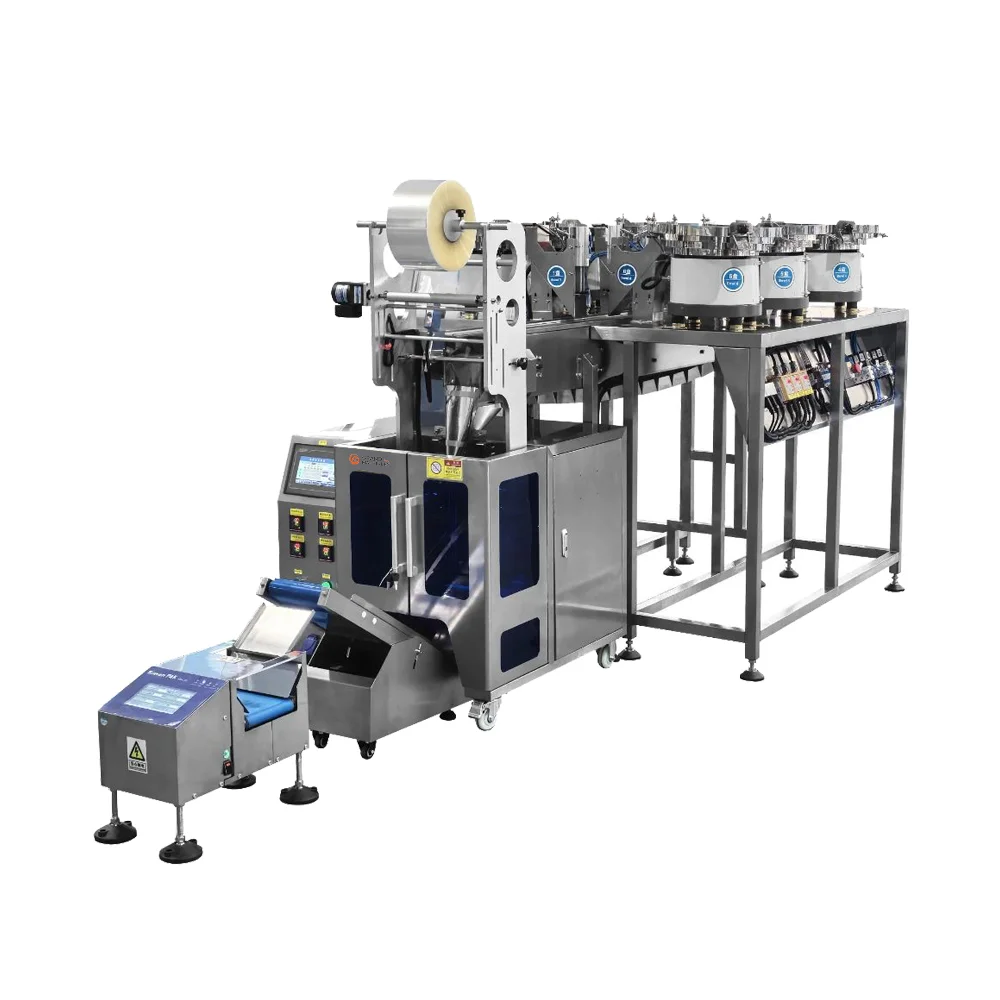
Changeover, cleaning and multi-SKU factors
If you run more than a handful of SKUs, changeover and cleaning time decide your real capacity more than top speed does. A machine filling 100 BPM but needing 45 minutes to clean between products will lose to an 80 BPM machine that cleans in 14. Write the cleaning procedure into the contract and time it during the factory acceptance test. Our GM16AE and GM12AE servo counting units are typical of the format buyers compare here; the GM280T6 covers the small-sachet variant of the same principle.
Integration items
Check the communication protocol (Modbus, Ethernet/IP or digital I/O), and confirm physical and signal interfaces with the bottle unscrambler upstream and the capping, desiccant and labeling stations downstream. Interface mismatches are cheap to fix at the drawing stage and expensive to fix on site.
What Comes Before and After the Gummy Counter
Upstream: unscrambling and product readiness
Bottles arrive nested and must be oriented before counting, and product must be dry, cool and free of surface tack. If your how vitamin gummies are made stages are not consistently delivering a dry, separated product, no counter will compensate.
Downstream: capping, desiccant, sealing and labeling
After filling, the bottle still needs a desiccant canister or sachet, a cap, an induction seal where required, and a label. Each station adds a failure mode and a queue, so design buffer lengths deliberately — a brief stop at the capping station must not back up into the counter and force a re-feed. The same applies to the desiccant inserter and the sticker labeling machine.
Standalone machine vs turnkey counting bottling line
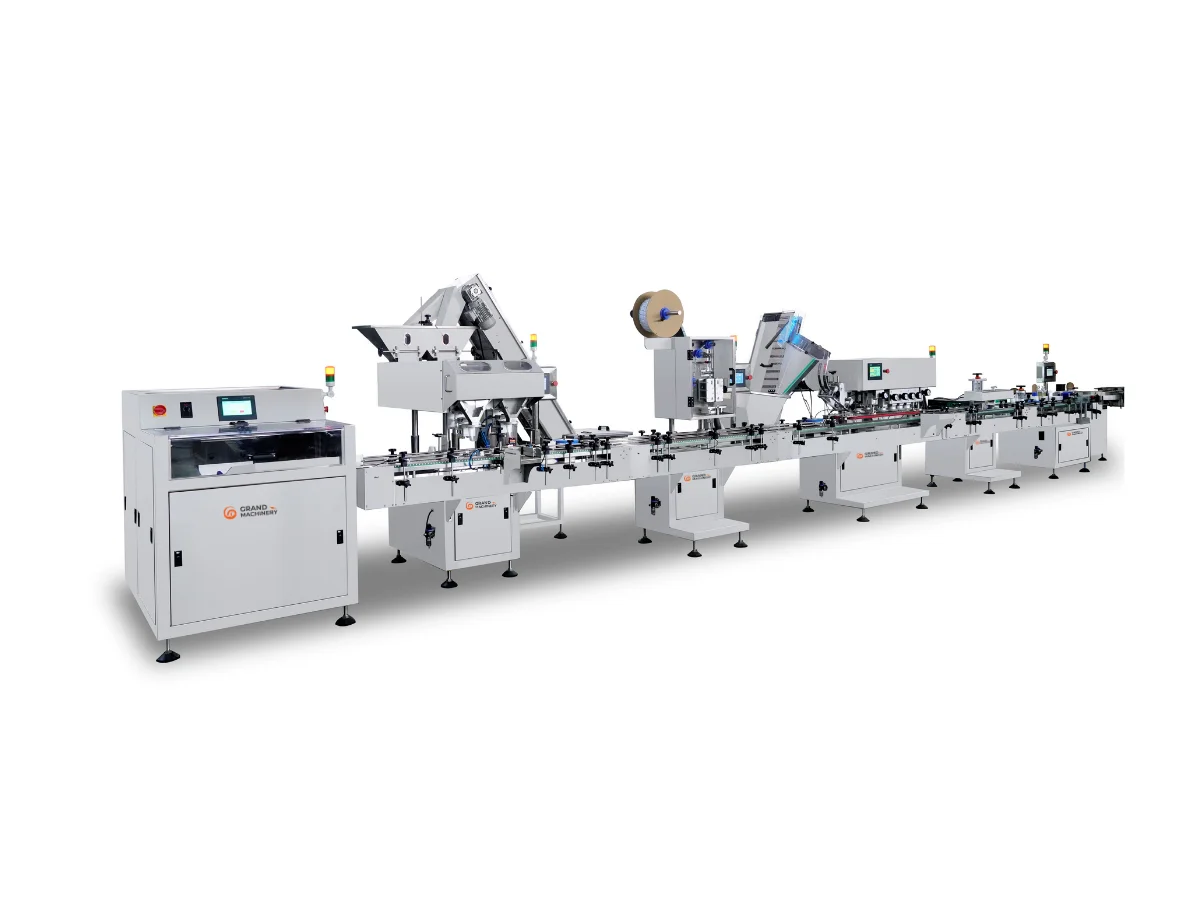
A standalone counter is right when you already have a line and only need to replace the filling step. Both floor-standing and vertical counting packing machine formats exist, and the choice usually comes down to bottle size and available floor space. If you are building from scratch, a turnkey counting bottling line removes the integration risk and gives you a single point of accountability for output guarantees.
Conclusion
A gummy counter is a simple idea — count pieces, one bottle at a time — executed in a machine that must cope with sticky, irregular, dust-shedding product at production speed. Get the coating match right, plan real capacity rather than rated capacity, and hold your supplier to a measured accuracy figure and a cleaning time.
Tell us your bottle size, the number of gummies per bottle and your target annual volume, and we will size the counting configuration and send you a layout and quotation.
FAQ
What does a gummy counter do?
A gummy counter counts individual gummy pieces and dispenses an exact number into each bottle or pouch. It replaces weight-based dosing, so the piece count printed on the label is the count actually filled.
How accurate is a gummy counter?
Production-grade optical counters are typically rated at ±0.02–0.03% of count. Real accuracy depends on product condition and cleaning discipline, so always ask how the figure was measured and over how many bottles.
Can a gummy counter handle sticky or sugar-coated gummies?
Yes, with the right configuration. Sticky and sanded gummies need PTFE or polished contact surfaces, anti-stacking rollers and dust extraction. Specify the coating type at quotation stage, because the channel set and amplitude settings differ.
How many bottles per minute can a gummy counter fill?
Standard machines run 40–80 bottles per minute, with high-configuration models reaching around 100 BPM. Plan production at roughly 80% of the rated figure to account for changeovers, cleaning and stoppages.
Gummy counter or weighing filler — which should I choose?
Choose a counter when the label states a piece count, which covers most bottled gummy vitamins. Choose a weigher when compliance is expressed as net weight or the product is irregular loose candy. Many lines run both.
Can one machine count both gummies and tablets?
Usually yes. Most counting heads handle a wide size range and both product types, but confirm the product size range and expect to retune amplitude and channel settings between soft gummies and tablets.