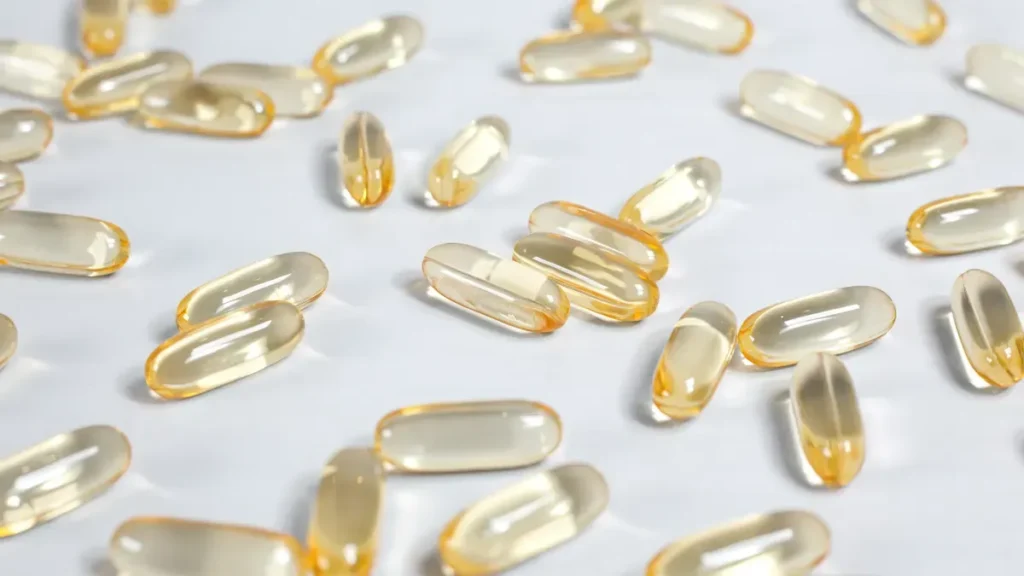
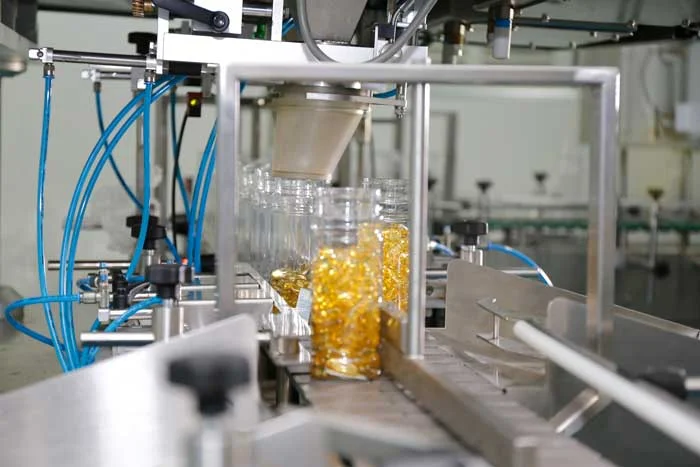
A softgel is a one-piece, hermetically sealed capsule. Manufacturers often craft it from gelatin or plant-based materials. This design holds liquid or semi-solid fills securely. Softgel capsules offer enhanced bioavailability for active ingredients. They provide precise dosing and shield oxygen-sensitive compounds from degradation. According to BCC Research, the global market for these capsules reached $7.4 billion in 2023. This value reflects their growing importance.
The softgel capsule manufacturing process demands precision at every stage. Gelatin quality directly influences shell strength and flexibility. This guide explains the complete journey, from raw material selection to final inspection. Readers will understand the technology behind this advanced dosage form.
Key Takeaways
- Softgels hold liquid or semi-solid ingredients. This form helps your body absorb them faster than tablets.
- The rotary die method makes softgels. It creates a strong seal that protects the contents from air and moisture.
- Gelatin and plant-based materials form the soft outer shell. Each type needs special care during production.
- Quality tests check for leaks, correct dosage, and proper breakdown. These tests ensure each softgel works safely.
- Manufacturers control temperature and humidity. This control prevents defects and keeps the softgels stable.
1. Introduction to Softgel Capsule Manufacturing
Softgel capsule manufacturing begins with two distinct components: the fill material and the shell. The fill forms the active core of the capsule. Most fills are oil-based solutions or suspensions. This choice protects ingredients that degrade in water. The viscosity of this fill material plays a critical role in the softgel encapsulation process. A fill that flows too freely may leak during sealing. A fill that is too thick may not pump evenly into the machine. Manufacturers must balance viscosity carefully for each formulation.
| Fill Category | Typical Viscosity |
|---|---|
| Marine oils | Low to medium |
| Fat-soluble vitamins | Low |
| Plant and seed oils | Low to medium |
| Oil-soluble actives | Medium |
| Suspensions | Medium to high |
The shell surrounds and protects this active core. Gelatin remains the most common shell material in softgel production. This protein provides strength, flexibility, and an excellent oxygen barrier. The gelatin shell also requires plasticizers to remain pliable. Glycerin and sorbitol serve this purpose well. Water acts as a third essential component during manufacturing.
| Shell Component | Typical Value |
|---|---|
| Water in wet shell formula | 30–40% w/w |
| Water in final dried product | 4–10% w/w |
| Non-volatile plasticizer | 15–30% w/w |
| Dry plasticizer to dry gelatin ratio | 0.3–1.0% w/w |
The industry standard for the dry gelatin-to-plasticizer ratio typically falls between 1.0:0.4 and 1.0:0.8. Adjustments toward higher plasticizer content become necessary when the fill is hydrophilic. Such fills tend to draw moisture from the shell. This interaction can affect capsule integrity over time.
Plant-based alternatives to gelatin continue gaining popularity. These options serve consumers seeking non-animal products. Common choices include:
- Carrageenan: Derived from red seaweed. Kappa carrageenan forms firm gels. Iota carrageenan produces softer, elastic gels. This material works well for softgel shells.
- Modified starch: Obtained from cassava root. This option is naturally gluten-free. It can also be non-GMO, halal, and kosher. Starch forms weaker films than gelatin but operates on standard rotary die equipment.
Each shell material demands specific handling during the manufacturing process. Temperature and humidity controls protect shell quality throughout production. The complete softgel capsule manufacturing journey transforms these raw materials into precise, hermetically sealed doses. This process serves the pharmaceutical industry and nutraceutical sector alike. Understanding these fundamentals helps formulators select appropriate materials for their specific product needs.
2. Why Choose Softgel Capsules? Benefits & Applications
The Rotary Die Method makes softgel capsules possible. This method stands as the industry gold standard. Liquid gelatin flows onto cooled drums to form thin, uniform ribbons. These ribbons feed into the rotary die machine. The machine simultaneously fills and seals each unit. This process creates a hermetic seal that protects the fill from oxygen and moisture. This encapsulation method works for both pharmaceutical products and dietary supplements.
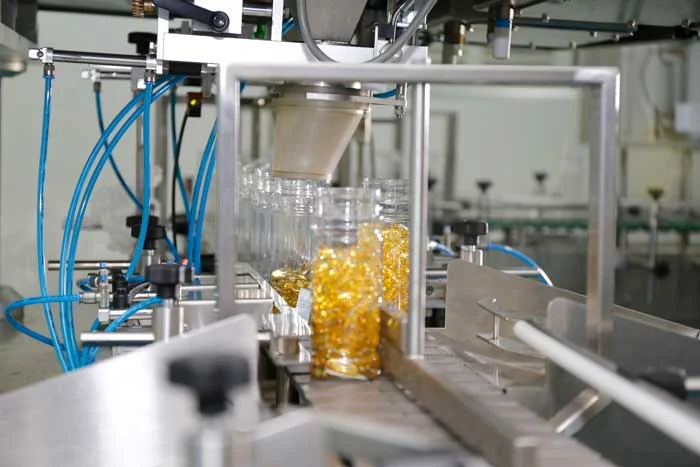
The softgel capsule manufacturing process follows six primary steps. Gelatin preparation mixes gelatin with plasticizers and water. Fill material preparation blends the active ingredient with a suitable vehicle. Encapsulation occurs in the rotary die machine. Drying removes excess moisture from the formed units. Inspection checks for defects. Packaging seals the finished product. Softgel production requires careful control of temperature and humidity throughout these steps.
The bioavailability advantage of soft gelatin capsules is well documented. Hard-shell capsules require a multi-step sequence. The solid must first disintegrate into fine particles. Then the particles must dissolve before absorption. This dissolution step often delays drug release.
Softgels are easily digested and have increased bioavailability. The shell material breaks down more quickly in the stomach. Hard units may require 30 to 60 minutes to break down. This faster shell disintegration leads to quicker drug release and absorption.
The physical state of the active ingredient explains this difference:
- Hard-shell units contain the active ingredient as a solid powder. The body must disintegrate and dissolve the solid before absorption. This multi-step sequence is often the rate-limiting factor.
- Softgels contain the active ingredient in a pre-dissolved state within a liquid vehicle. Once the gelatin shell ruptures, the active ingredient releases instantly in an absorbable form. This leads to quicker onset and more direct delivery to the bloodstream.
This contrast shows why the manufacturing method matters. The ability to hold pre-dissolved actives is a direct result of the encapsulation technology.
Market data confirms the value of this dosage form. The vitamin and dietary supplement segment holds a 23.2% revenue share of the softgel capsules market in 2025. The nutraceutical companies segment projects a compound annual growth rate of 10.0%.
| Metric | Value |
|---|---|
| Revenue share of vitamin and dietary supplement segment in softgel capsules market (2025) | 23.2% |
| Projected CAGR of nutraceutical companies segment in softgel capsules market | 10.0% |
Patient compliance also improves with softgels. The reasons are clear:
- Easy to swallow compared to large tablets
- Mask unpleasant taste and odor of active ingredients
- Better patient compliance with daily regimens
- Protect drugs from environmental factors
- Suitable for controlled drug release formulations
The drying stage occurs after encapsulation. Newly formed units move into tumble dryers. These dryers rotate slowly, allowing air to circulate around each unit. The process removes excess moisture from the shell. The final water content drops from 30-40% to 4-10%. This step ensures the unit reaches the correct hardness and flexibility. Final inspection follows drying. Automated systems check each unit for defects. Leaks, air bubbles, and shape deformities trigger rejection. This quality check ensures only intact units reach packaging. The softgel manufacturing process demands precision at every stage.
3. Key Ingredients Used in Softgel Capsule Manufacturing
The quality of softgel capsules depends heavily on ingredient selection. Each component serves a specific purpose in the final product. The gelatin shell provides structure and protection. The fill material delivers the active ingredient. Both must work together to create a stable dosage form.
3.1 Gelatin Sources
Gelatin remains the primary shell material in softgel manufacturing. Manufacturers choose from several sources based on product requirements and target markets:
- Bovine gelatin: Sourced from cows. This type offers strong, durable consistency. Pharmaceutical and nutraceutical products commonly use it.
- Porcine gelatin: Sourced from pigs. This option provides excellent gelling properties and a smooth texture.
- Fish gelatin: Serves as an alternative for Halal or Kosher markets. This source produces a lighter, more flexible shell.
- Vegetarian gelatin: Plant-based options include pectin, tapioca, and carrageenan. These suit vegan and vegetarian consumers.
The choice of gelatin source affects the manufacturing process. Each type responds differently to temperature and humidity. Manufacturers must adjust their process parameters accordingly.
3.2 Carrageenan as a Plant-Based Alternative
Carrageenan has gained regulatory approval as a gelatin alternative. The FDA permits its use under 21CFR172.620. This regulation allows carrageenan as a fat replacer, stabilizer, thickener, binder, and texturizer. The FDA has also classified it as generally recognized as safe (GRAS).
The European Food Safety Authority (EFSA) lists carrageenan as E407. This authorization includes a temporary acceptable daily intake of 75 mg/kg body weight per day. The UK Food Standards Agency categorizes it as an emulsifier, stabilizer, thickener, and gelling agent.
Regulatory bodies including the FDA and EFSA confirm that undegraded carrageenan is safe for use in food and supplements. This approval encompasses softgel capsules. Manufacturers can confidently use carrageenan for vegetarian formulations.
3.3 Water Content and Shell Stability
Water plays a critical role in the gelatin shell. Freshly encapsulated softgels contain 35–40% water in the shell. This high moisture content makes the units soft and pliable. However, this state lacks physical stability.
The drying process deliberately reduces water content to approximately 10%. This target represents the typical finished softgel shell. At this moisture level, the capsule achieves proper hardness and flexibility. The shell maintains its shape and protects the fill material effectively.
3.4 Quality Control Tests
Quality assurance begins with raw material testing. Manufacturers verify that each ingredient meets specifications before production starts. The finished soft gelatin capsules undergo several key tests:
- Disintegration testing: This test measures how quickly the capsule breaks apart in digestive fluids. Softgels typically disintegrate faster than tablets or hard-shell capsules.
- Dissolution testing: This test measures the rate at which the active ingredient releases from the capsule. The results confirm that the fill material becomes available for absorption.
- Content uniformity testing: This test verifies that each capsule contains the correct amount of active ingredient. Consistent dosing is essential for pharmaceutical products.
These tests ensure that every batch meets quality standards. The manufacturing process must produce consistent results across thousands of units.
3.5 Environmental Controls
Temperature and humidity control are essential throughout the softgel capsule manufacturing process. High humidity can cause the gelatin shell to absorb moisture. This absorption leads to shell deformation or microbial growth. Low humidity can make the shell brittle and prone to cracking.
Manufacturers maintain strict environmental controls in production areas. Temperature typically remains between 20–25°C (68–77°F). Relative humidity stays below 35% during encapsulation and drying. These conditions protect the gelatin shell and ensure product stability.
The combination of quality ingredients, precise process control, and rigorous testing produces reliable softgel capsules. Each element of the manufacturing process contributes to the final product’s performance.
4. Step-by-Step Softgel Capsule Manufacturing Process
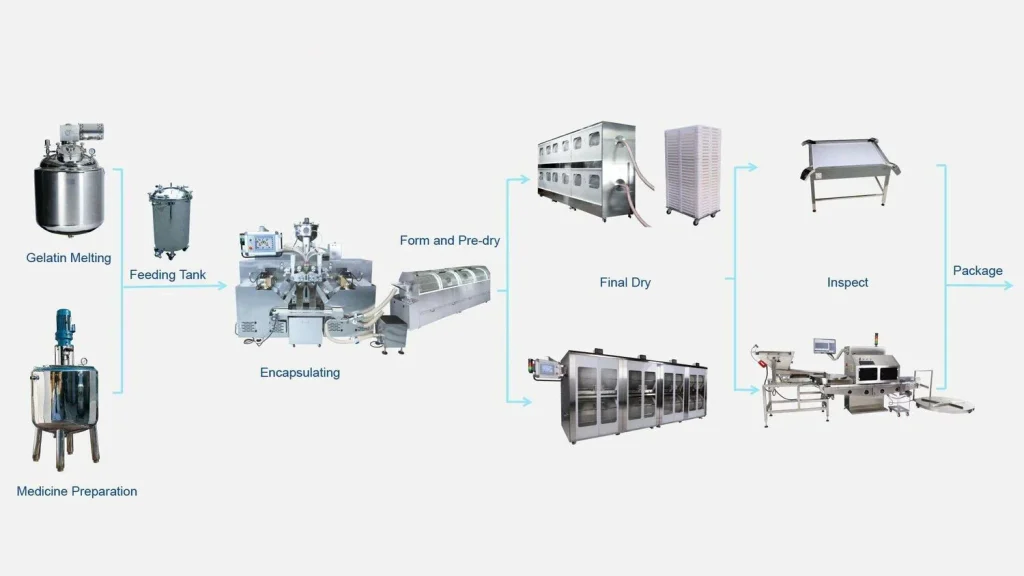
The softgel capsule manufacturing process transforms raw materials into finished dosage forms. This process differs from tablet and hard-shell capsule production. Softgels handle liquid formulations directly. The active ingredient exists in a pre-dissolved state. This eliminates the need for disintegration and dissolution steps. Ingredients with poor solubility benefit from this approach. Substances with low melting points also work well. They remain stable in the liquid fill. The rotary die method enables this softgel production. Modern machines produce over 300,000 softgels per hour. The manufacturing process requires careful control of all parameters.
4.1. Gelatin Preparation (The Shell)
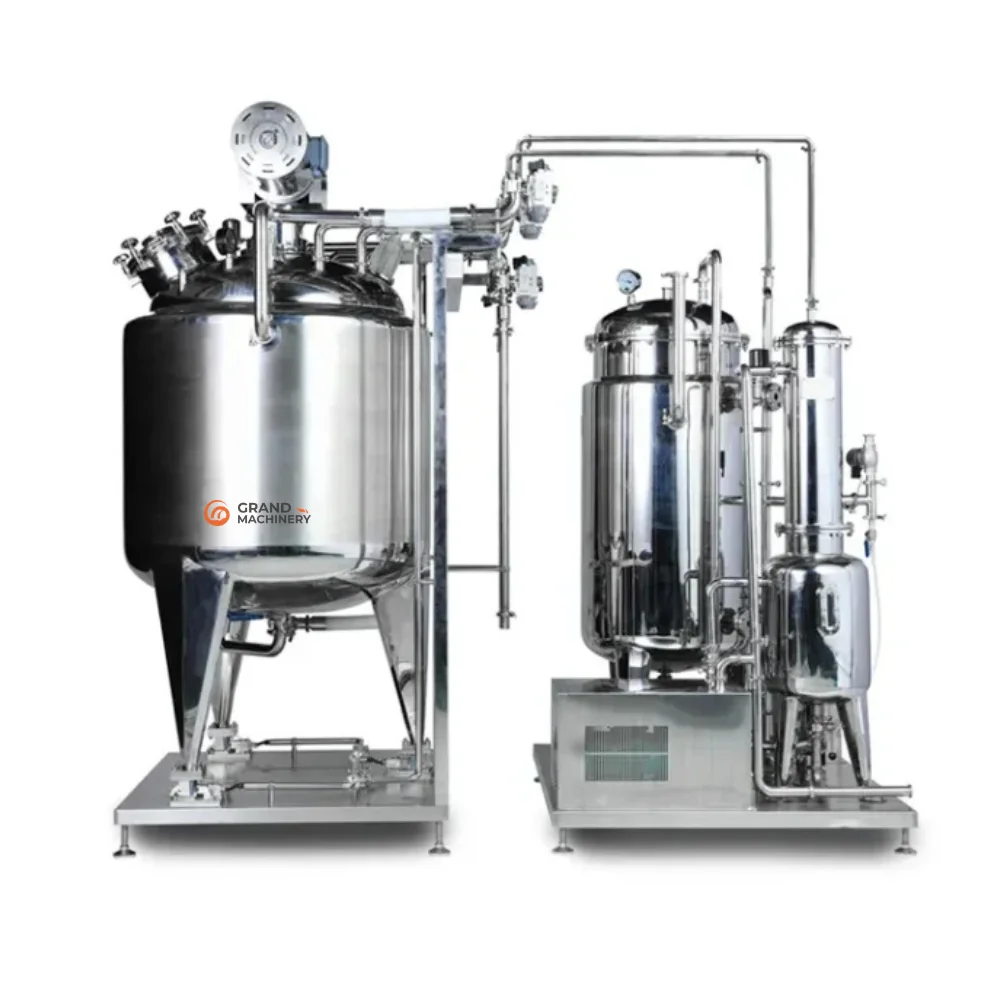
Gelatin preparation begins with melting the raw material. The target temperature range is 60°C to 70°C. This range ensures correct viscosity and consistency. The melted gelatin then mixes with plasticizers and water. The mixture forms a homogenous solution. The solution flows onto cooled drums. This creates thin, uniform ribbons. These ribbons feed directly into the rotary die machine.
Several defects can occur during ribbon formation. Improper ribbon thickness leads to seam leakage or pinholes. Low wedge temperature produces a stiff ribbon. This causes poor sealing. High wedge temperature reduces sealing efficiency. Gelatin viscosity variation causes thickness deviation. The shell must remain uniform. These issues directly affect final capsule quality. The gelatin preparation process requires careful monitoring of temperature and viscosity. Drying follows the encapsulation step. The drying process removes excess moisture from the shell. The final water content drops to the target range. This ensures the capsule achieves proper hardness.
4.2. Fill Material Formulation (The Core)
While the shell is being prepared, the fill — the active ingredient suspended in oil, or dissolved in a compatible liquid — is formulated in a separate tank. Because softgel fills must not contain water that would attack the gelatin shell, oils and oil-soluble ingredients are the natural home for many actives. The fill is blended to a consistent viscosity and kept free of air, then metered to the machine so that every capsule receives an identical dose.
Consistent viscosity matters more than most buyers expect. If the fill is too thick, it may not flow evenly into the metering pump; if too thin, it can leak or make the seal uneven. A well-calibrated fill, by contrast, fills the shell cleanly and protects the seal’s integrity through the entire softgel capsule manufacturing process.
4.3. Encapsulation Process (Rotary Die Technology)
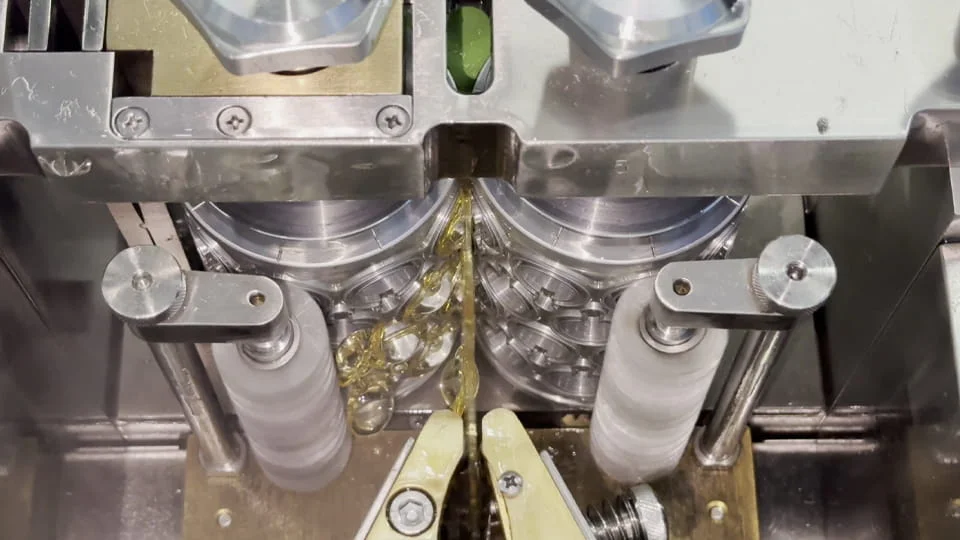
Encapsulation is the heart of the line, and it relies on the rotary die method. Two continuous ribbons of gelatin film are cast from the prepared mass and drawn between a pair of rotating dies. As the dies meet, they form matching half-shells, the metered fill is injected between them, and the dies seal the two halves together in a single synchronized motion — creating a softgel that is filled and hermetically sealed before it ever leaves the die.
The precision of this stage determines the accuracy of every dose and the strength of every seal. Well-engineered rotary die equipment keeps the ribbon thickness even, the fill dose consistent and the seam clean. It is here that production speed, waste and final capsule quality are largely decided, which is why selecting the right encapsulation machine is the single most important equipment decision in the whole softgel capsule manufacturing setup.
4.4. Drying and Curing
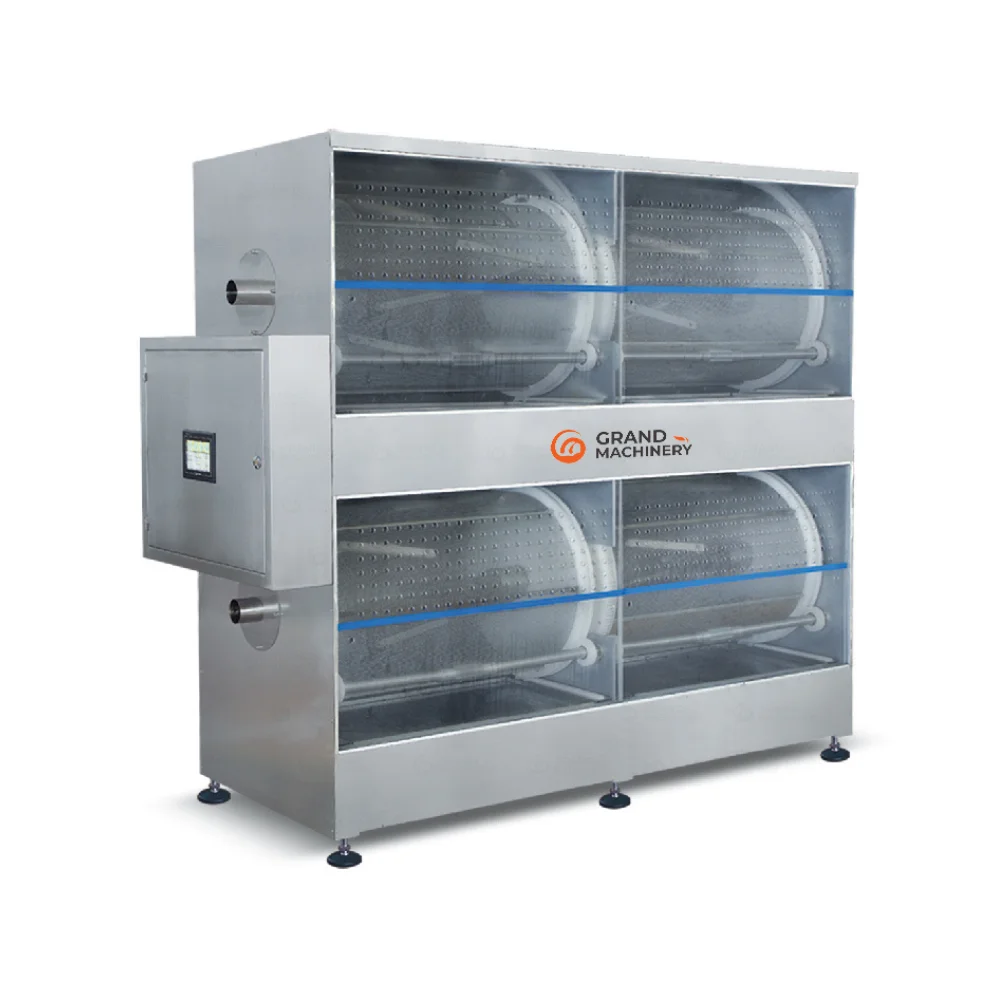
Freshly formed softgels are still soft and contain excess moisture, so they move directly from the die to a tumble dryer. Here they are gently rotated in a warm, controlled airflow that removes surface moisture and hardens the shell. Drying prevents the softgels from sticking to one another and gives the shell the firmness it needs to survive packaging and handling.
Drying must be carefully managed — the goal is to reach an optimal residual moisture, not to dry the capsule until it becomes brittle. Temperature, airflow and residence time are all balanced so the softgel retains the slight flexibility that protects the fill inside. Many producers pass the units through a series of tumble dryers or a drying tunnel to reach the right moisture profile without over-drying the surface.
4.5. Inspection, Sorting, and Polishing
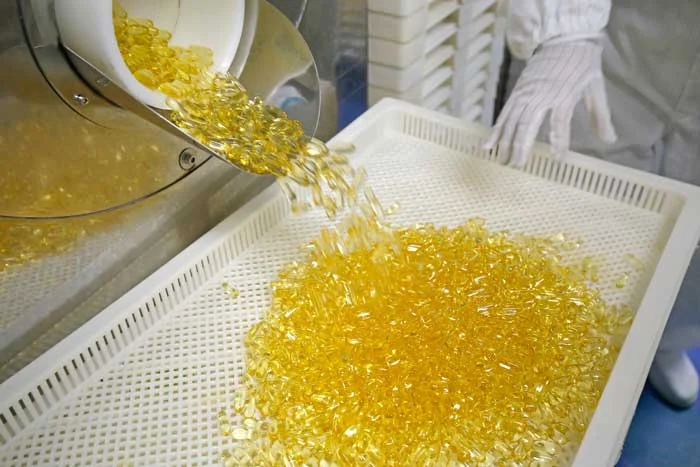
The final stage turns the dried softgels into a clean, uniform batch ready for packaging. Automated inspection systems check every capsule for defects such as leaks, dents, misshapen shells or inconsistent fill, ejecting any unit that fails. Sorting then groups the softgels by size and shape, and a polishing step removes residual oil or film residue from the surface so the finished capsules are clean and visually consistent.
This quality pass matters not only for appearance but for the reliability buyers expect. A softgel that looks clean and uniform signals a controlled, professional process — and it also protects your line downstream, since only sound capsules should reach the packaging stage. When these five stages run in sequence under consistent control, the result is a hermetically sealed, precisely dosed softgel ready for bottling, blistering or pouch packaging.
5. Quality Control and Compliance in Softgel Capsule Manufacturing
Quality control is essential for producing consistent, safe, and compliant softgel capsules. Manufacturers must monitor both the gelatin shell and fill material throughout the softgel capsule manufacturing process.
5.1 Rupture Test
The USP 32 standard specifies a rupture test for softgel capsules using water as the medium. Apparatus 2 operates at 50 rpm, with a 15-minute limit. Capsules should rupture within this period, with specific retesting requirements for units that fail the initial test.
5.2 Content Uniformity
Content uniformity testing verifies that each softgel contains the correct amount of active ingredient. Initial testing typically uses 10 units, with each unit required to fall within 85.0%–115.0% of the label claim and an RSD of no more than 6.0%.
If additional testing is required, 20 more units are tested. For the full 30-unit test, no more than one unit may fall outside 85.0%–115.0%, no unit may fall outside 75.0%–125.0%, and the RSD must be no more than 7.8%.
5.3 Environmental and Visual Inspection
Temperature and humidity directly affect gelatin quality. During drying, the temperature should be around 25°C with 20%–25% RH. Production and storage areas generally require 20°C–30°C and 30%–50% RH.
| Process | Temperature | Humidity |
|---|---|---|
| Softgel Drying | 25°C | 20%–25% RH |
| Production & Storage | 20–30°C | 30%–50% RH |
Final inspection checks for leaks, air bubbles, deformation, and other defects. Automated inspection and rejection systems help ensure that only intact capsules proceed to packaging. Complete batch records also support regulatory compliance and product traceability.
6. Common Challenges in Softgel Capsule Manufacturing and How to Avoid Them
Several common problems can affect softgel quality and production efficiency.
6.1 Leaking Softgels
Leakers are among the most common defects. They can result from weak seals, cracks, excessive drying, fill pressure, die misalignment, incorrect wedge temperature, or inaccurate pump timing.
The fill formulation can also affect sealing performance. Ingredients such as lecithin, pastes, and herbal powders may create additional challenges. Maintaining the correct gelatin viscosity, sealing pressure, drying conditions, and equipment settings is therefore essential.
6.2 Gelatin Cross-Linking
Gelatin cross-linking can prevent the capsule shell from dissolving properly, affecting drug release and product performance. It may be triggered by certain aldehydes, ketones, oxidizing agents, metal ions, or other reactive ingredients.
Prevention focuses on selecting suitable gelatin and excipients, controlling environmental conditions, and using appropriate packaging. Specialized gelatin grades, such as cross-linking-resistant formulations, can also improve stability.
Regular quality checks and environmental monitoring help identify problems early and maintain consistent softgel production.
7. Conclusion: Choosing the Right Softgel Capsule Manufacturing Equipment
Choosing the right softgel capsule manufacturing equipment is critical for achieving consistent quality, reliable output, and efficient production. Modern rotary die machines combine precise dosing, automated controls, and stable capsule forming to meet demanding production requirements.
Important equipment features include:
| Feature | Description |
|---|---|
| Sensor-Controlled Feeding | Maintains consistent material flow and reduces waste. |
| High-Precision Piston Pump | Provides accurate and consistent fill dosing. |
| Teflon-Coated Injectors | Reduces sticking and maintenance requirements. |
| Servo Drive | Improves timing accuracy and production stability. |
| Automatic Die Alignment | Maintains precise die positioning and reduces downtime. |
| Micro-Lubricant Technology | Reduces sticking, cleaning, and equipment wear. |
| Cold Air System | Helps prevent gelatin from sticking during production. |
| PLC/Touchscreen Controls | Provides easy control of capsule size, fill volume, and production speed. |
Reliable equipment must maintain precise control from gelatin preparation and filling to sealing, drying, and inspection. This is especially important for pharmaceutical and nutraceutical applications where dosage accuracy and product consistency are essential.
With the right combination of equipment, materials, and quality control, manufacturers can produce high-quality softgel capsules efficiently while meeting applicable industry standards.
Contact Grand Machinery for guidance on softgel capsule manufacturing equipment selection. Our team can evaluate your specific needs and recommend appropriate solutions for your production goals.
FAQ
How long does the softgel capsule manufacturing process take?
The complete process spans several days. Encapsulation itself runs quickly, with modern machines producing over 300,000 units per hour. The drying stage requires the most time. Fresh capsules contain 30-40% water. Reducing moisture to the target 4-10% range typically takes 24 to 72 hours in tumble dryers.
What causes softgel capsules to leak?
Leaking usually traces back to sealing problems. Weak seals develop from incorrect wedge temperature or misaligned die lands. Fill composition also matters. Lecithin, pastes, and herbal powders interact poorly with standard gelatin formulations. Over-drying creates brittle shells prone to cracking. Proper parameter monitoring prevents most leaker issues.
Can softgels contain water-based ingredients?
Yes, but formulators must exercise caution. Water migrates from the fill into the gelatin shell. This migration softens the shell and compromises capsule integrity. Manufacturers adjust the plasticizer ratio when working with hydrophilic fills. Higher plasticizer content compensates for moisture draw. Oil-based fills remain the standard choice for most softgel products.
How do manufacturers test softgel quality?
Quality control involves several pharmacopeial tests. Disintegration testing confirms the capsule ruptures within 15 minutes in water. Dissolution testing measures active ingredient release rates. Content uniformity testing verifies each unit contains 85-115% of the labeled dose. Visual inspection catches leaks, air bubbles, and shape deformities before packaging.
What is the shelf life of softgel capsules?
Most softgel products maintain stability for 24 to 36 months when stored properly. Temperature should remain between 20-30°C. Relative humidity must stay between 30-50%. Exposure to light accelerates degradation. Proper packaging with desiccants and blister packs extends product life. Each formulation requires stability testing to establish its specific expiration date.